- घर
- हमारे बारे में
- उत्पाद
- समाधान
- केस अध्ययन
- संसाधन
- संपर्क करें
Steel plate flatness defects account for 15-25% of welding failures in pressure vessel and wind tower fabrication. Studies show proper leveling equipment reduces material rejection rates by up to 40% while improving coating adhesion and dimensional accuracy across heavy manufacturing operations.
If you want to eliminate flatness problems in thick plate processing, you need to understand leveling machine types, working principles, and capacity specifications.
In today's article, we will explain the main types of leveling machines, their technical specifications, and selection criteria for steel fabrication. This guide helps you achieve consistent flatness for wind tower shells, pressure vessels, and structural steel projects.
A leveling machine is precision metal forming equipment that eliminates internal stresses and surface irregularities in steel plates through controlled multi-point bending. Modern leveling systems use roller arrays with hydraulic or mechanical adjustment to achieve flatness tolerances down to 0.5mm per meter.
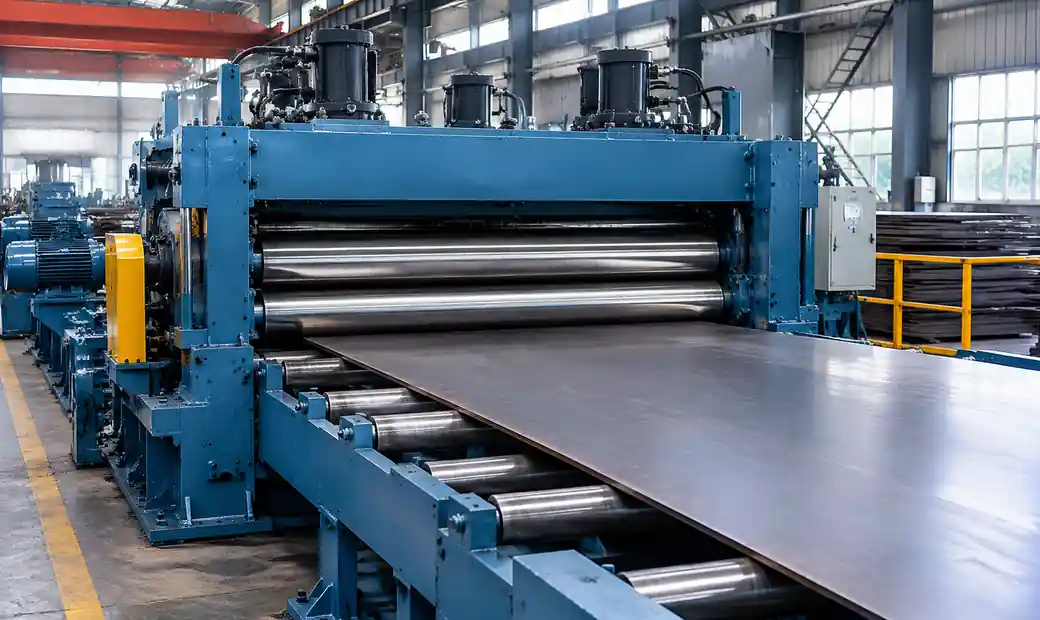 Industrial leveling machine processing steel plates in manufacturing facility
The equipment processes plates from 3mm to 100mm thickness, removing coil set, edge wave, center buckle, and residual stresses that cause warping during cutting or welding operations.
Industrial leveling machines range from compact 5-roll systems for sheet metal to heavy-duty 13-roll or 21-roll units processing 80mm-thick plates for wind tower and pressure vessel applications. You can integrate leveling into production lines before cutting, after plasma cutting, or as standalone precision correction.
Leveling operates through alternating plastic deformation. Steel plates pass through staggered upper and lower rolls that bend the material beyond its yield point in opposite directions.
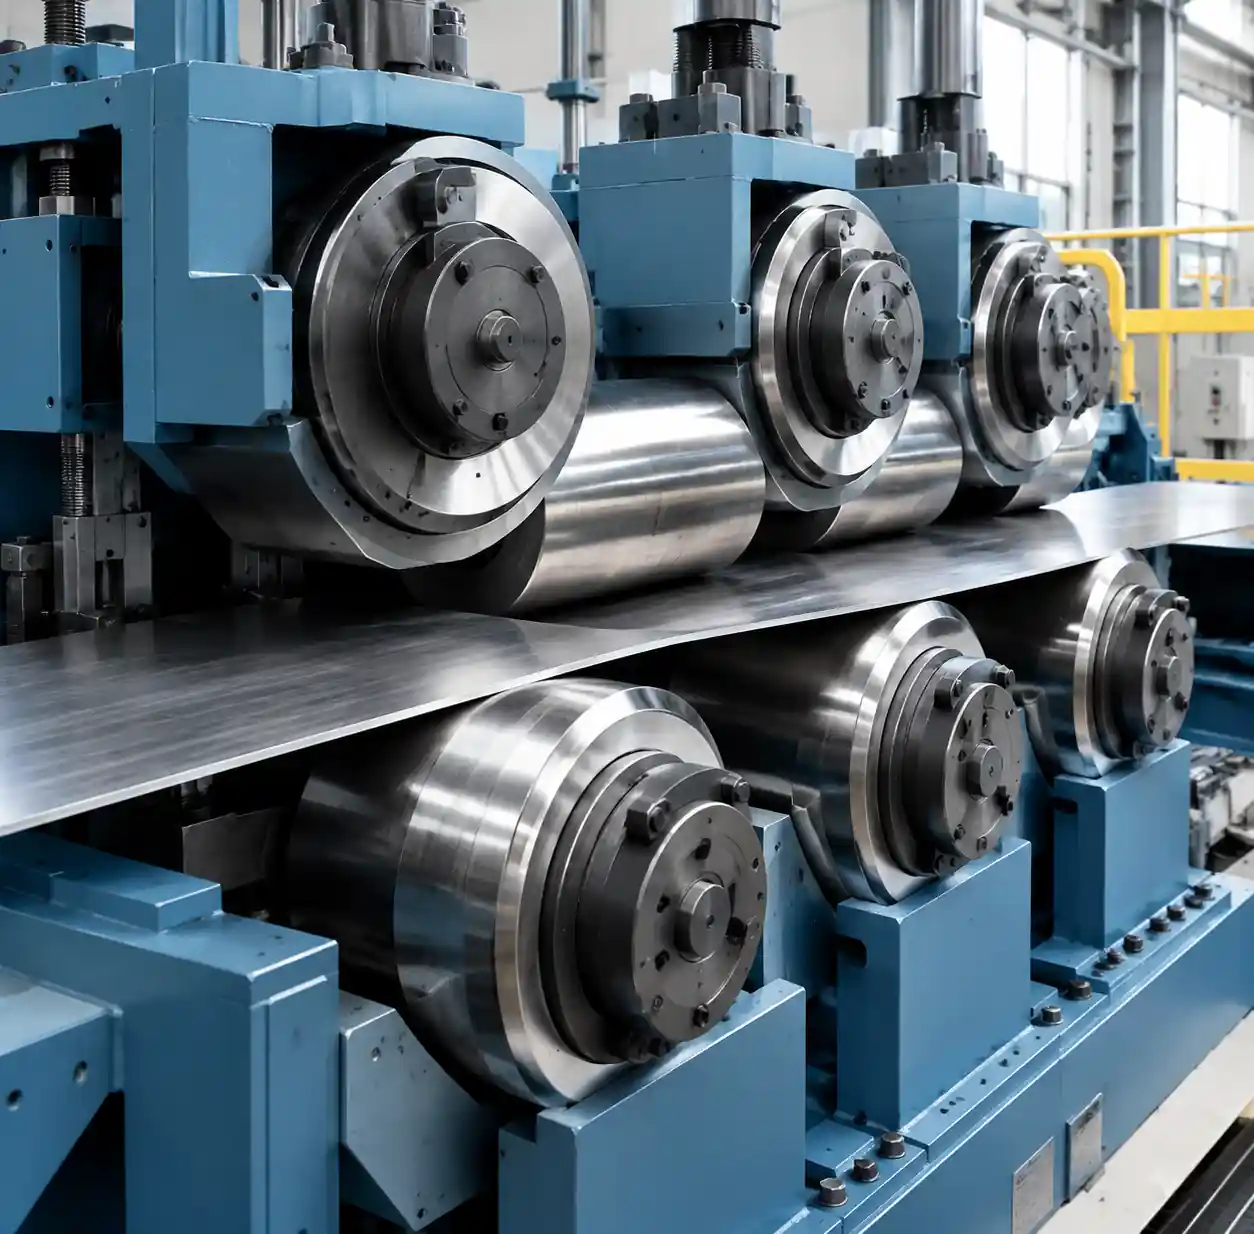 Leveling machine roll configuration showing alternating bending process
The process works in three stages. First, entry rolls create initial downward bend removing coil set. Second, intermediate rolls apply alternating up-down bending that eliminates internal stresses across the plate width. Third, exit rolls apply final straightening with gradually reduced bending amplitude.
Each bending cycle exceeds the material's yield strength, permanently deforming high spots while low areas receive less deformation. After multiple bending cycles, the entire plate reaches uniform flatness. Roll pressure, spacing, and penetration depth determine final flatness results.
For thick plates above 40mm, hydraulic systems provide 300-600 tons of leveling force. Precision servo positioning adjusts roll gaps to ±0.01mm, ensuring consistent results across varying material grades and thickness ranges.
Entry-level systems use 5 or 7 working rolls suitable for thin to medium plates up to 25mm thickness. These compact machines handle general fabrication work where flatness requirements stay within ±1.5mm per meter.
Specifications:
Choose 5-7 roll systems when processing construction steel, general fabrication plates, or applications where moderate flatness suffices and initial investment must stay minimal.
Medium-duty systems deploy 11 or 13 working rolls for improved flatness on plates from 8mm to 50mm. Additional bending cycles remove more internal stress and handle materials with higher yield strength.
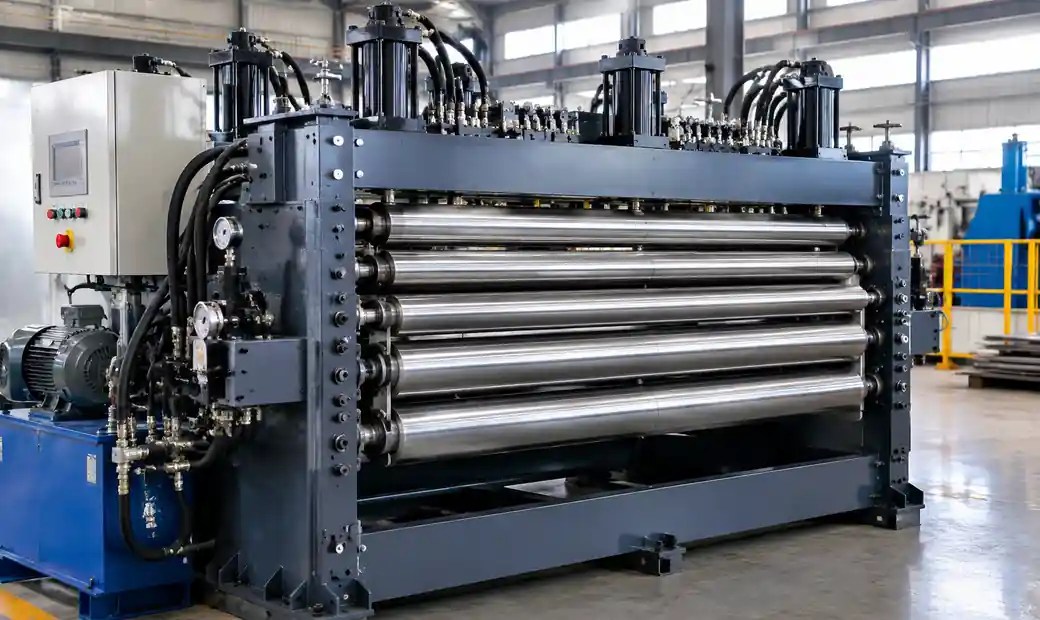 11-roll or 13-roll precision leveling machine for medium-duty applications
These machines serve wind tower fabrication, shipbuilding, and boiler manufacturing where welding quality depends on precise flatness. Hydraulic adjustment enables processing different thicknesses without manual roll changes.
Technical advantages:
For operations processing multiple plate grades and thicknesses daily, 11-13 roll systems provide flexibility without sacrificing precision.
Heavy-duty leveling machines feature 17 to 21 working rolls specifically engineered for extra-thick plates from 20mm to 100mm. These systems deliver flatness within ±0.3mm per meter on high-strength steels including Q460, S460, and wear-resistant grades.
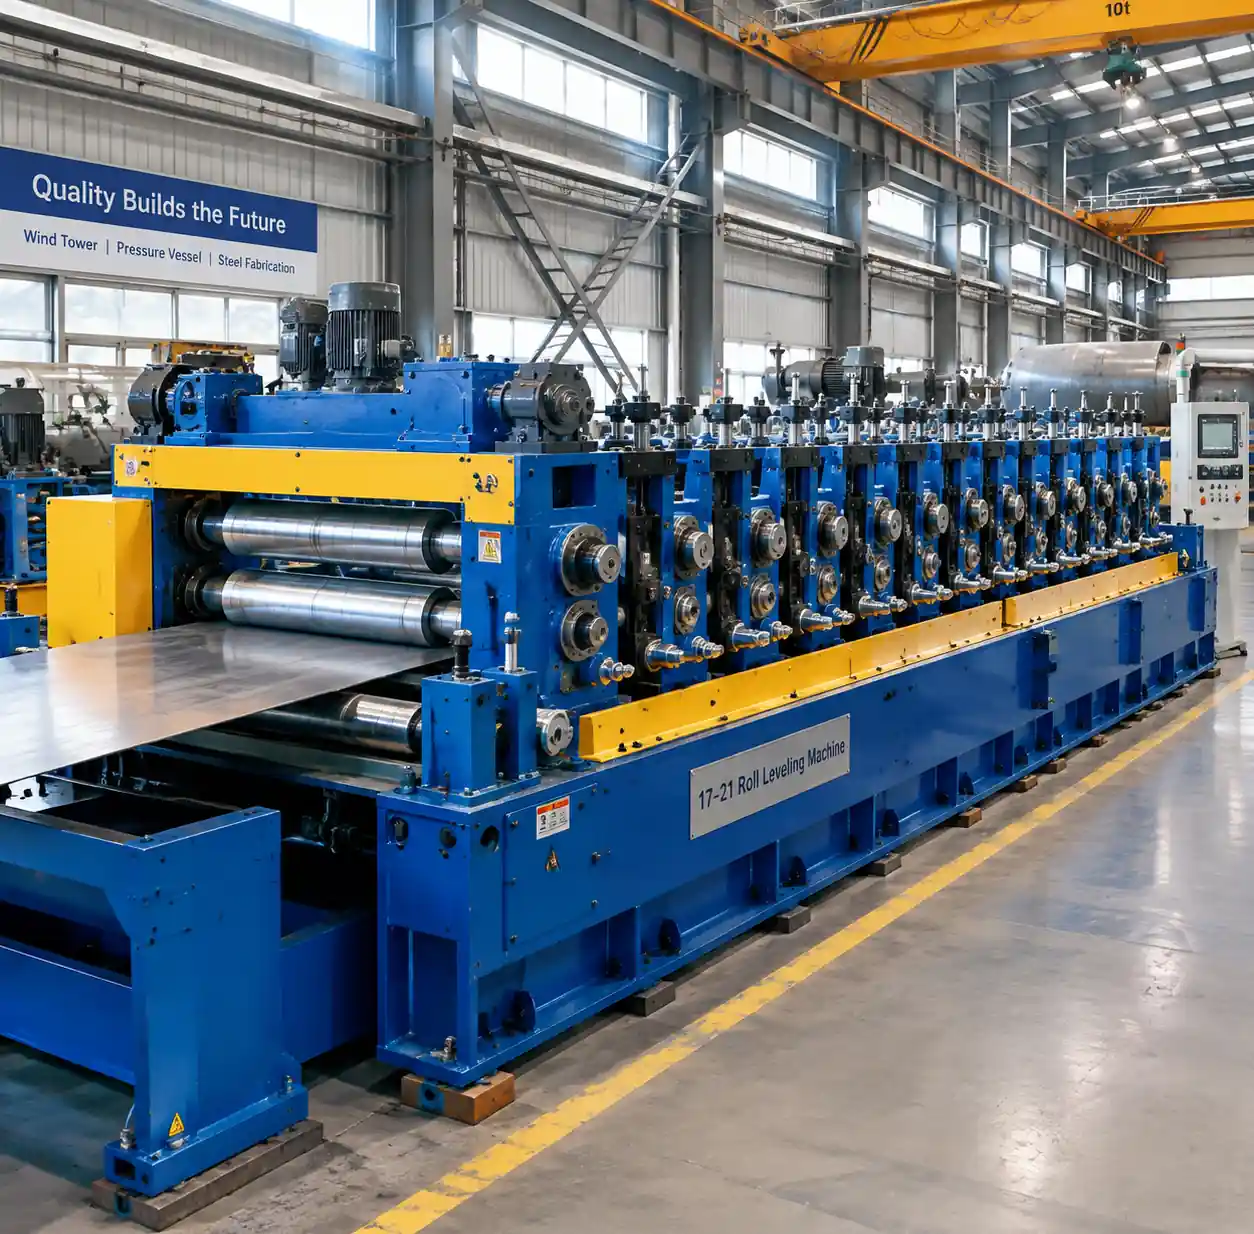 Heavy-duty 21-roll leveling machine for thick plate processing
Roll arrays with 17+ contact points distribute leveling force across shorter plate segments, enabling uniform stress relief in thick sections. Hydraulic pressure reaches 600 tons on 21-roll machines processing 80-100mm wind tower base sections.
Heavy-duty capabilities:
Wind tower manufacturers and pressure vessel fabricators processing ultra-thick plates require 17-21 roll systems to meet stringent flatness specifications before plate rolling operations.
| Parameter | 5-7 Roll Systems | 11-13 Roll Systems | 17-21 Roll Systems |
|---|---|---|---|
| Thickness Range | 3-25mm | 8-50mm | 20-100mm |
| Flatness Tolerance | ±1.5mm/m | ±0.5mm/m | ±0.3mm/m |
| Coil Set Removal | Moderate | Good | Excellent |
| Yield Strength | Up to 355MPa | Up to 460MPa | Up to 690MPa |
| Initial Cost | Baseline | 40-60% higher | 2-3x baseline |
| Best Applications | General fabrication | Wind towers, vessels | Heavy plate, premium work |
Mechanical systems use gearboxes and drive shafts to rotate all rolls simultaneously at fixed speed ratios. These cost-effective machines suit continuous production with consistent material specifications.
Operators adjust roll pressure through threaded mechanisms or hydraulic cylinders while material feeds at constant speed. Mechanical drives provide reliable operation in high-volume environments processing standardized plate grades.
Hydraulic servo systems offer independent control over roll positioning, pressure, and feed speed. CNC interfaces store programs for different materials, enabling rapid changeover between plate specifications.
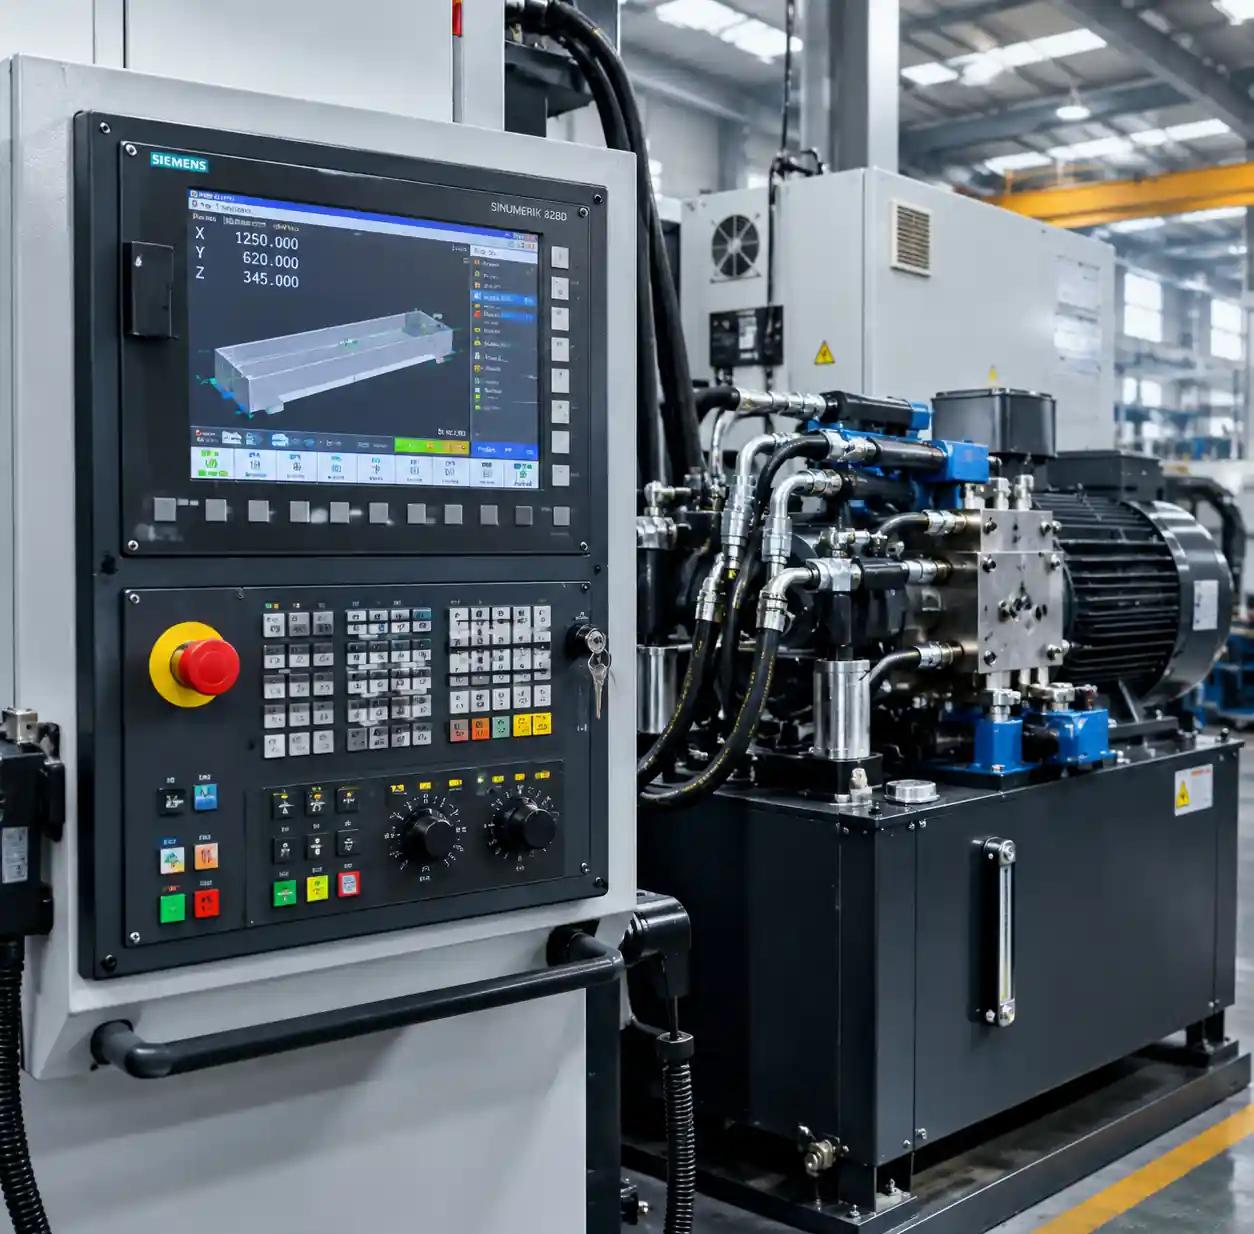 CNC hydraulic servo control panel for leveling machine
Servo-controlled entry and exit pinch rolls match leveling speed to upstream and downstream equipment. Real-time pressure monitoring adjusts force distribution across the plate width, compensating for thickness variations.
Servo advantages:
For fabricators running multiple plate grades, servo systems recover initial investment through reduced setup time and improved first-pass yield rates.
Wind tower production demands flatness within ±0.5mm per meter on 20-120mm plates. Insufficient leveling causes dimensional drift during cylinder forming and weld seam misalignment.
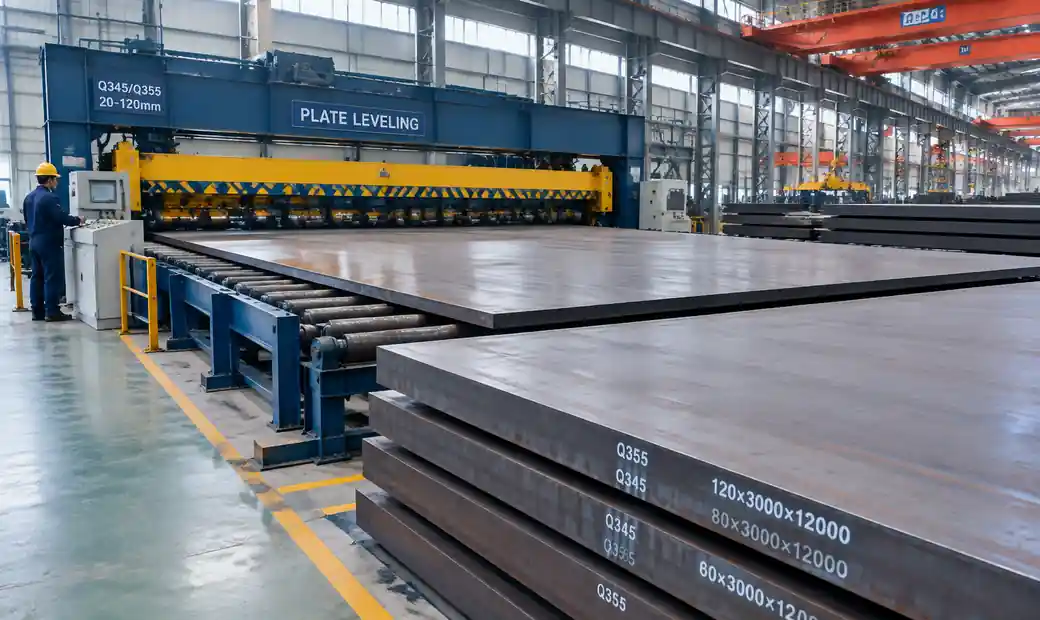 Steel plates for wind tower manufacturing being processed on leveling machine
EZHONG leveling machines process Q345 and Q355 tower sections up to 5000mm width, removing residual stresses that cause springback during plate rolling. Precision leveling reduces weld preparation time by 25-35%.
Pressure vessel codes require flat surfaces for radiographic inspection. Vessels above 100 bar need flatness within ±0.3mm per meter on 30-80mm shell plates.
Bridge girder fabrication and construction steel benefit from leveling before CNC cutting, improving cut quality and reducing torch height adjustment requirements.
| Method | Flatness Achieved | Thickness Range | Equipment Cost | Production Speed |
|---|---|---|---|---|
| Roller Leveling | ±0.3-0.5mm/m | 3-100mm | High | Continuous |
| Flame Straightening | ±2-5mm/m | 10-200mm | Low | Batch/manual |
| Press Braking | ±1-3mm/m | 5-50mm | Medium | Batch |
| Stretch Leveling | ±0.5-1mm/m | 0.5-6mm | High | Continuous |
Roller leveling provides the best balance of precision, throughput, and thickness capability for heavy plate fabrication. Flame straightening handles thicker plates but lacks precision and automation. Stretch leveling excels on thin materials but cannot process structural plate thicknesses.
Larger roll diameters reduce surface marking on thick plates. Machines processing 60-100mm plates require 200-300mm diameter rolls. Roll spacing ranges from 150mm on entry rolls to 100mm at exit, with closer spacing improving stress relief on high-strength materials.
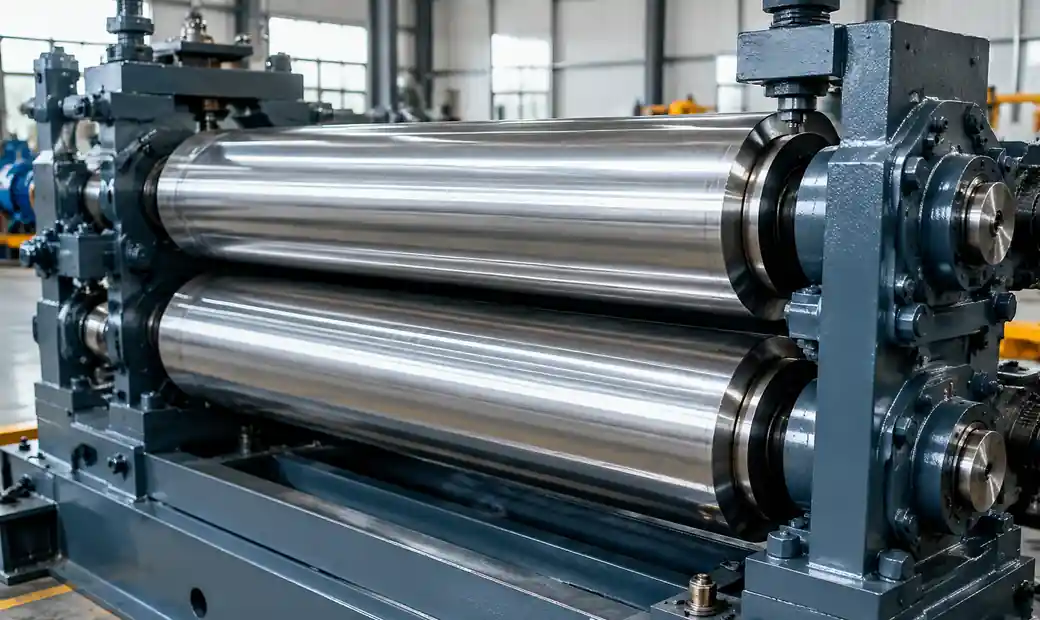 Close-up of leveling machine rolls showing diameter and spacing configuration
Select working width based on your largest plate dimensions plus 100-200mm margin. Wind tower fabricators need 4000-5000mm capacity while standard structural work operates with 2500-3000mm width.
Leveling force requirements increase with plate thickness and yield strength. Calculate required force as: Force (tons) ≈ (Thickness mm × Width mm × Yield Strength MPa) / 1000. Specify hydraulic systems with 20-30% capacity margin above calculated requirements.
Modern leveling machines integrate into automated production flows with entry/exit conveyors connecting to shearing, cutting, or plate rolling equipment. For wind tower lines, leveling positions between shearing and plate rolling machines, reducing cylinder diameter variation.
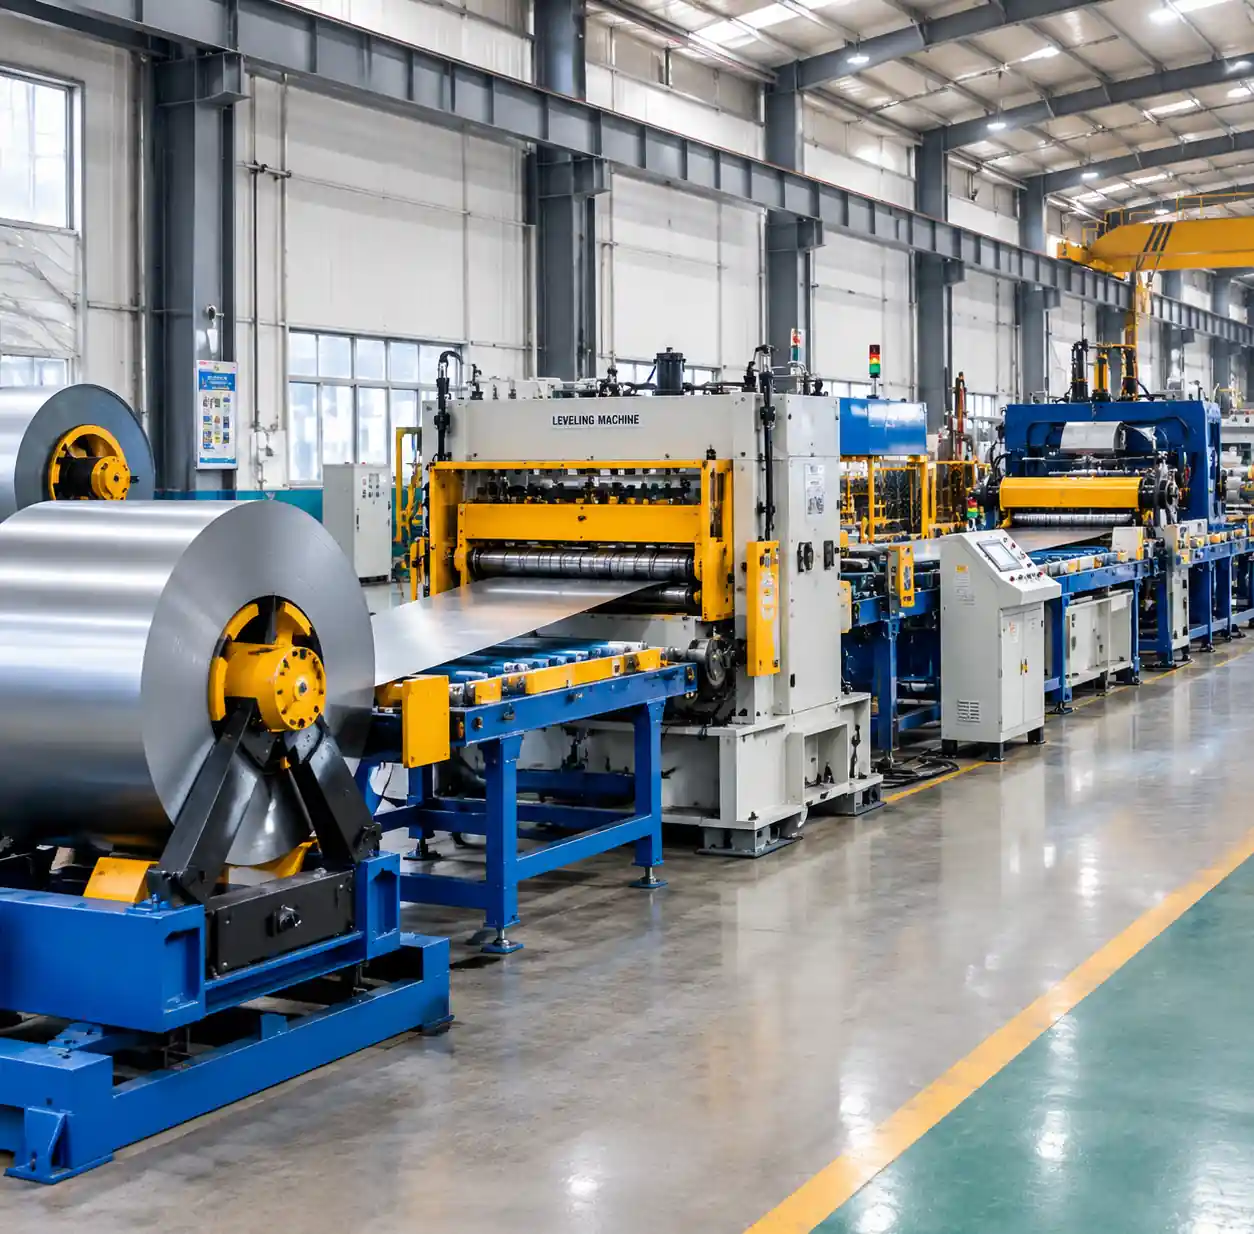 Leveling machine integrated into automated plate processing production line
Typical ROI periods range from 18-36 months for facilities processing 5000+ tons annually. Investment delivers 30-40% reduction in weld rejection, 25% faster assembly fit-up, and improved coating adhesion. Fabricators with consistent flatness problems on plates above 30mm see fastest returns on 11-roll or heavier systems.
What flatness can leveling machines achieve?
Precision leveling systems achieve ±0.3 to ±0.5mm per meter on thick plates. Actual results depend on material grade, thickness, and initial condition. Heavy-duty machines with 17+ rolls deliver tightest tolerances on plates 40-100mm thick.
How does plate thickness affect leveling?
Thicker plates require more rolls, larger roll diameters, and higher hydraulic pressure. Machines must generate sufficient force to exceed material yield strength throughout the plate cross-section. This is why 5-roll systems max out around 25mm while 21-roll machines handle 100mm plates.
Can leveling machines process high-strength steel?
Yes, but higher yield strength requires increased hydraulic pressure and additional roll passes. Q460 and S460 grades need 11-13 roll minimum. Wear-resistant steels above 500 HBW may require specialized roll materials and surface treatments.
What causes edge wave after leveling?
Edge wave results from insufficient roll penetration at plate edges or improper roll crowning. Modern machines use individually adjustable edge rolls or crowned center rolls that apply more pressure at edges, eliminating wave on wide plates.
How fast do leveling machines operate?
Feed speeds range from 2-8 meters per minute depending on thickness and material. Thin plates under 15mm process faster while 60-100mm plates require slower speeds for effective stress relief. Servo systems optimize speed automatically.
Do leveling machines work on as-rolled or heat-treated plates?
Both. As-rolled plates typically have coil set requiring leveling before fabrication. Heat-treated plates may develop distortion during quenching that leveling removes. Some manufacturers level before heat treatment then again afterward for critical applications.
Leveling machines eliminate flatness defects that compromise welding quality, dimensional accuracy, and production efficiency in heavy plate fabrication. Proper equipment selection based on thickness range, material grades, and flatness requirements directly impacts downstream operation success.
For wind tower, pressure vessel, and structural steel fabrication, precision leveling reduces rejection rates while improving assembly fit-up and weld quality. Investment in appropriate roll count and drive system configuration delivers measurable returns through reduced rework and faster throughput.
EZHONG manufactures heavy-duty leveling machines from 5-roll to 21-roll configurations, processing plates up to 100mm thickness and 5000mm width. Our hydraulic servo systems deliver ±0.3mm flatness tolerance on high-strength steels for wind energy and pressure vessel industries. With over 60 years of metal forming equipment expertise, EZHONG provides complete leveling solutions integrated with plate rolling and pipe making production lines.
Contact us today for custom leveling machine specifications and capacity calculations tailored to your plate processing requirements.